A pump seal on a press line rarely fails without warning. It fails quietly, over days or weeks, as friction and temperature slowly climb, right up until the moment it doesn’t. By the time anyone notices, the line is down, the shift crew is standing around a hot pump instead of running board, and the plant is looking at a repair window measured in hours, not minutes.
This isn’t a rare scenario. It’s one of the most common ways a small, preventable mechanical issue turns into a full production loss at a wood products mill, and it’s exactly the failure mode our spare parts data confirms: wood products mills are, by a wide margin, our most active spare parts customers. The plants that run these systems hardest already know reliability isn’t optional. This post is about the mechanics behind why, and what actually closes the gap.
Pressing, drying, and resin curing all depend on consistent, high-temperature heat delivered through a closed-loop thermal oil system. A single heater circulates thermal fluid to multiple points across the press line, holding a steady temperature that steam or direct-fired alternatives struggle to match at this scale.
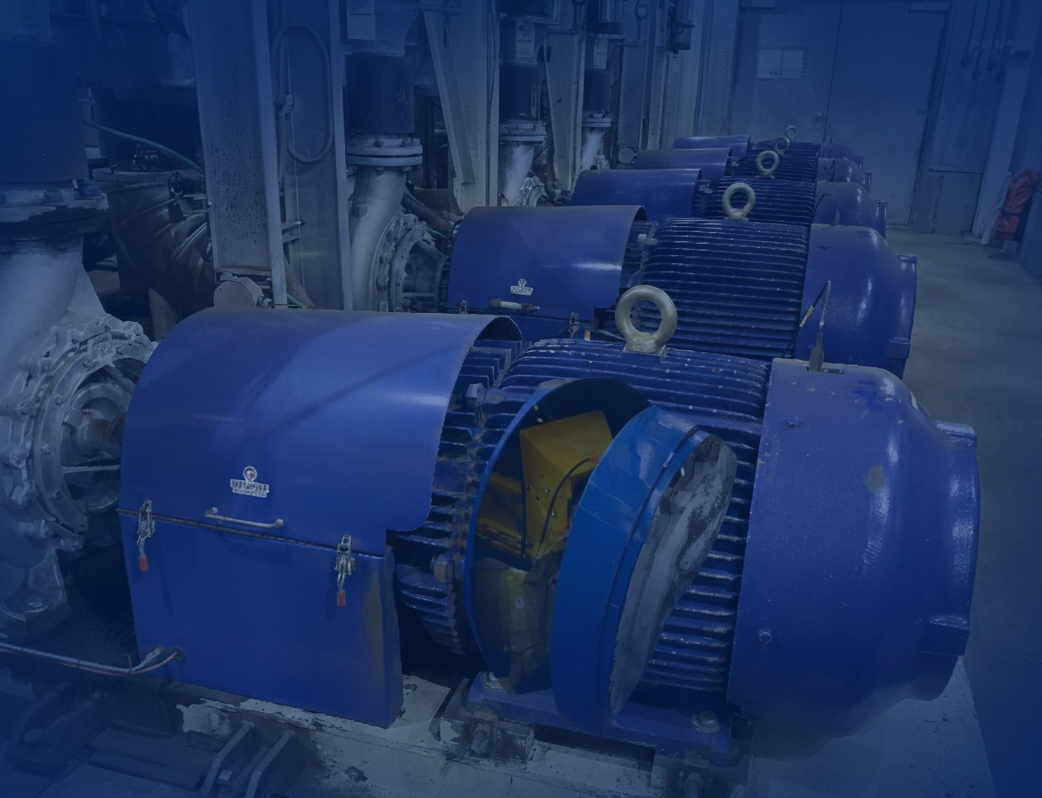
The pumps that circulate that fluid run continuously across long production cycles, often 24/7. That’s exactly why PumpGuard was originally built around wood products applications in the first place, mills don’t get the luxury of a slow ramp-up or a forgiving maintenance window. The system either keeps running or the line stops.
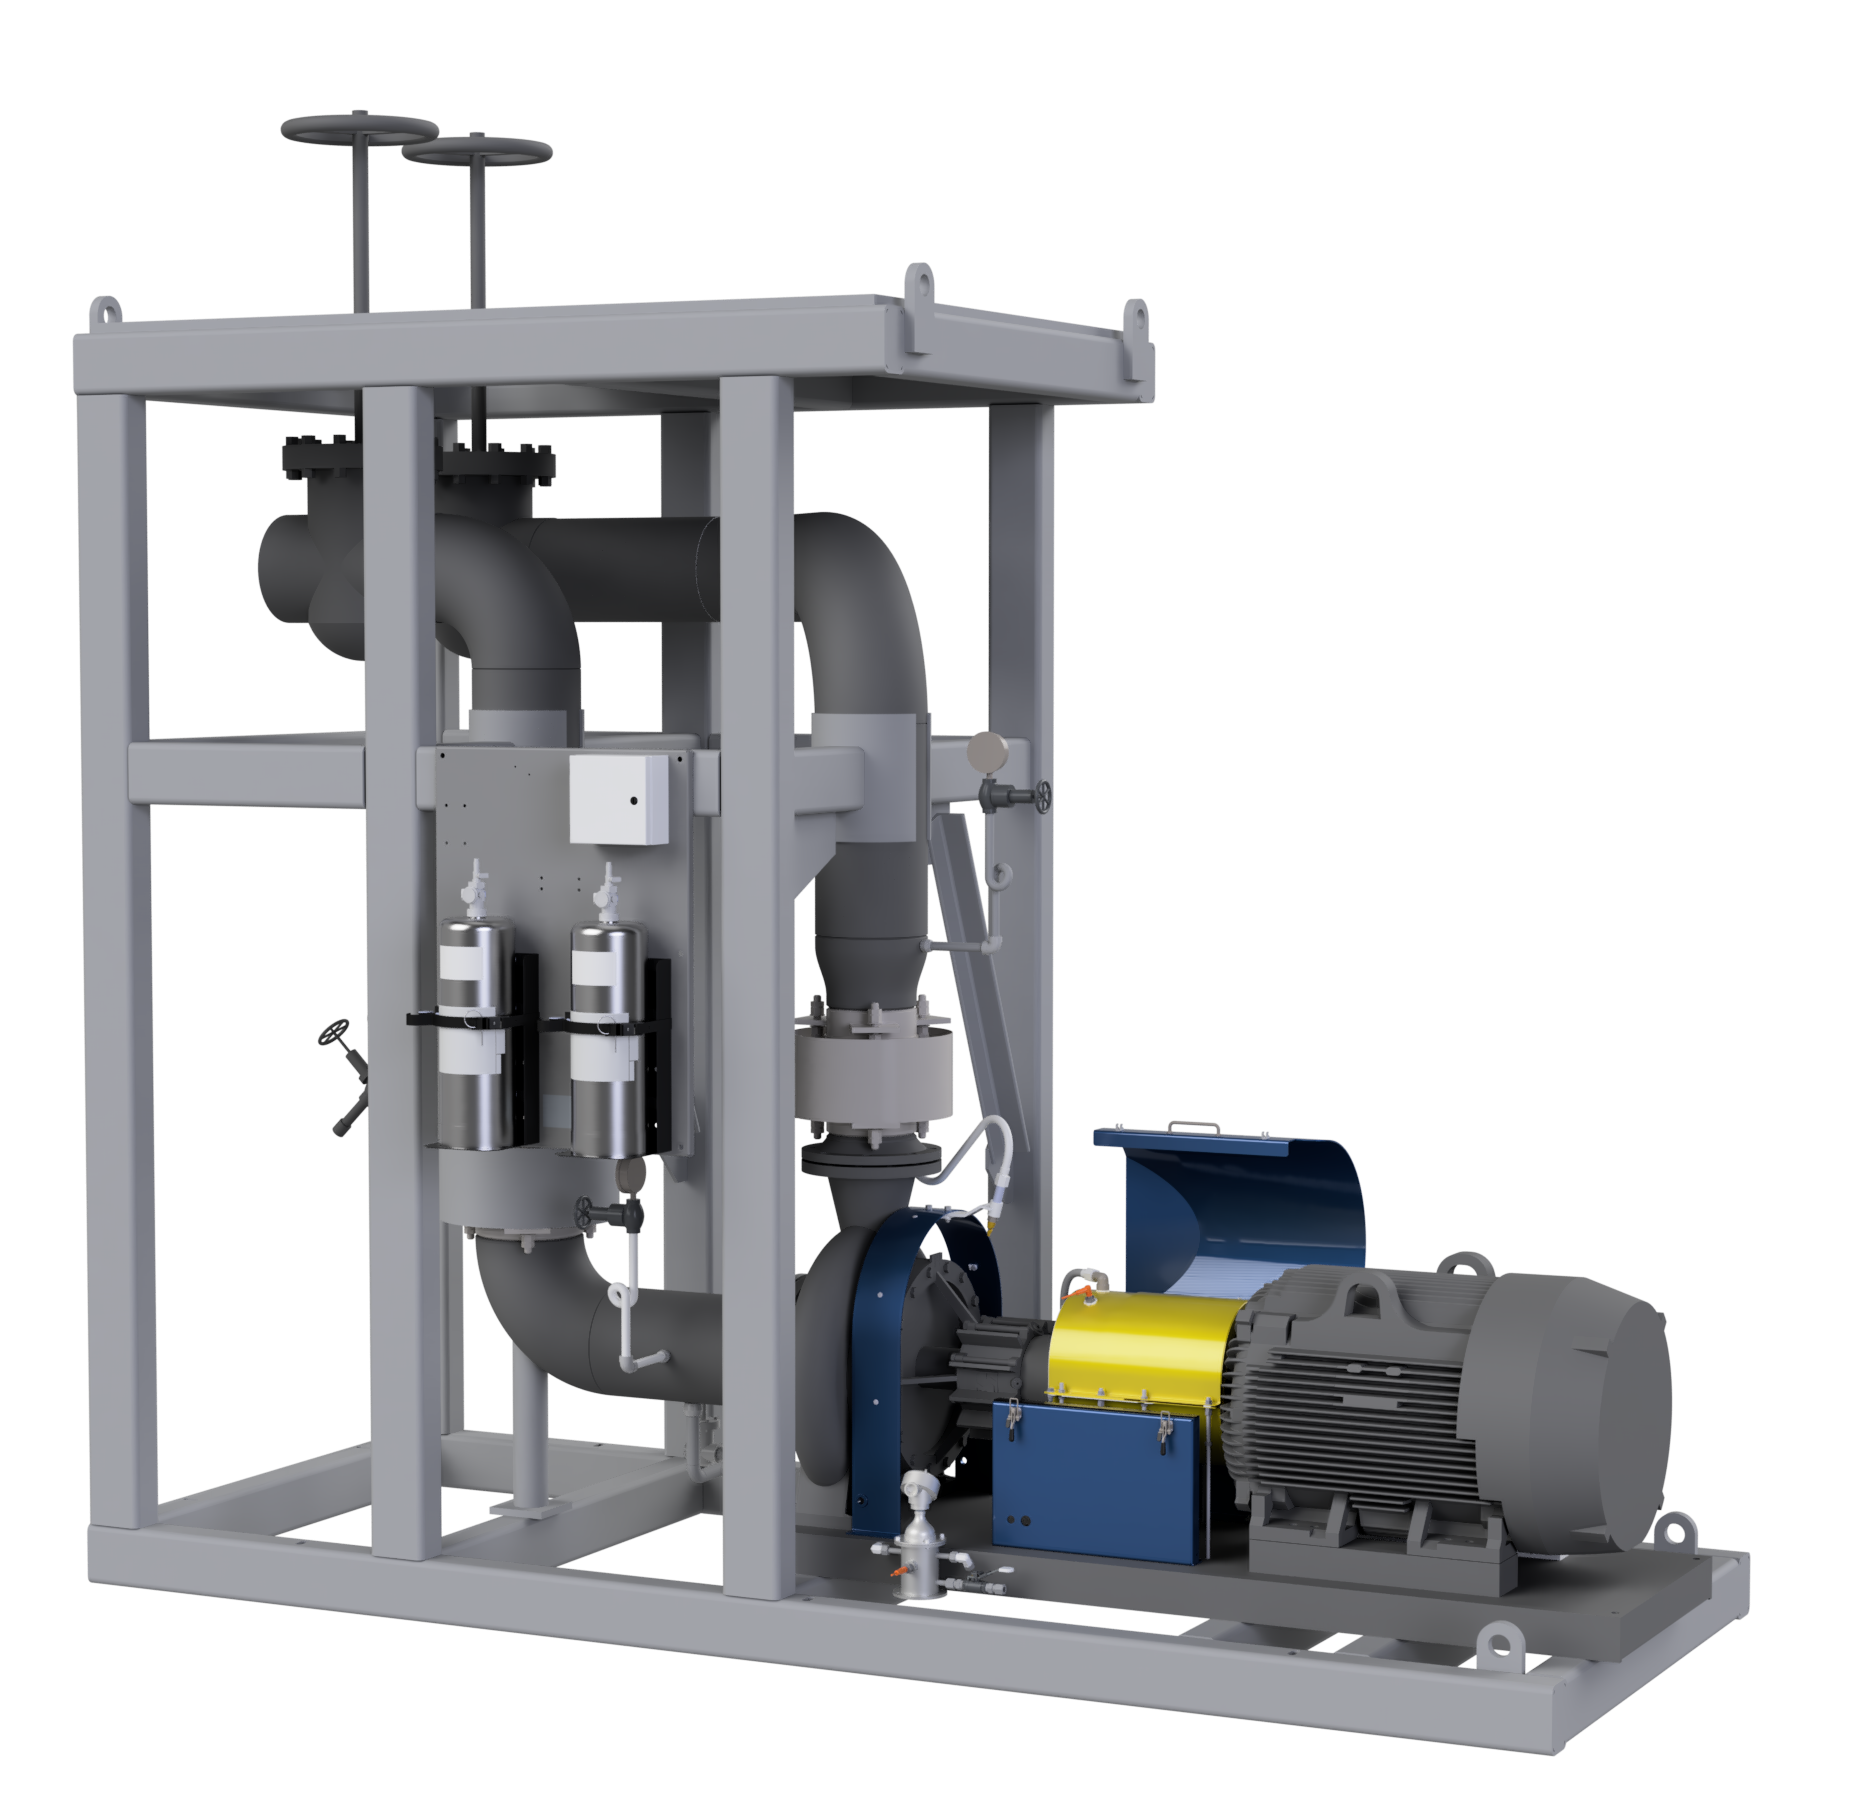
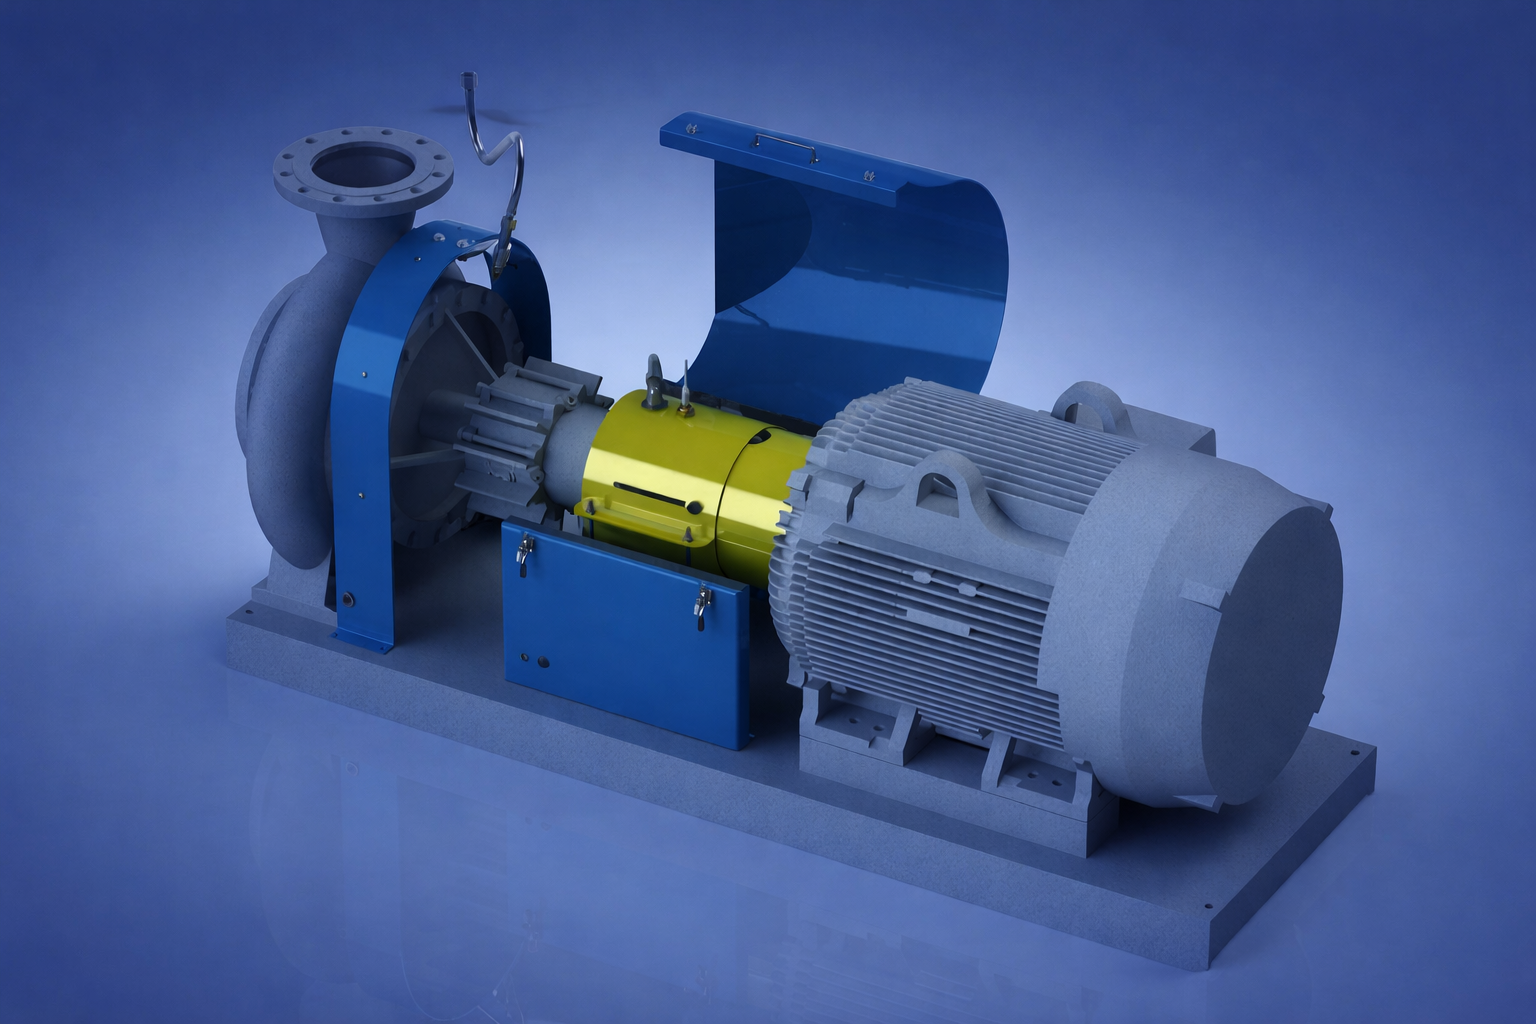
At the center of PumpGuard is a dual guard housing, a design that’s patent pending. The outer air housing captures cooling air directly from the pump motor’s own fan and routes it over the seal, extending seal life before wear ever becomes a failure. The inner guard housing covers the motor coupling and seal, isolating it from surrounding airflow to prevent a fire from spreading, while creating a closed, contained volume built specifically for suppression.
Detection is entirely mechanical. PumpGuard doesn’t rely on plant power to sense or respond to a fire, which matters on a press line where an electrical fault is often part of the same failure chain that starts a seal fire in the first place. Multiple pumps can also be interconnected to a central monitoring HMI panel for plant-wide visibility, but that’s a convenience layered on top, not a dependency the system needs to function.
It’s also worth being direct about what PumpGuard isn’t: a replacement for the fire suppression system already protecting your plant. It’s built to layer on top of that system, adding a dedicated, pump-specific level of protection that a general suppression system was never designed to provide at the seal itself.
Two configurations are available, and the right one depends on how much of the pump area needs coverage. The base PumpGuard package protects the seal itself, forced air cooling, mechanical detection, and active suppression, all contained at the coupling guard.
PumpGuard+ extends that coverage to the pump’s volute casing with an additional cowling, sensing line, and foam nozzle, backed by a second, independently zoned foam canister. That means the system doesn’t just respond generically, it detects and suppresses at the specific location of the fire, seal or volute, rather than treating the whole pump area the same way.
8 warning signs your thermal fluid pump seals show before failure, and exactly what to check during your next planned shutdown. Built specifically for panel and board production lines.
A thermal fluid pump failure rarely stops just one component. Because press cycles and resin curing depend on consistent heat across the entire line, a single pump issue can halt production for a full shift or longer while the system is inspected and repaired.
And unlike a quick part swap, getting a press line back to full operating temperature after an unplanned shutdown adds its own time on top of the repair itself. The board that was mid-cycle when the line went down is often a loss too. None of this shows up on the maintenance ticket, but all of it shows up on the production report.
This isn’t a market we’re new to. Wechsler Technologies provides equipment built by engineers with deep, hands-on expertise in process heating, designed around one goal: protect your people, extend the life of your equipment, and get more out of your process heating environment while keeping your plant safer. We’ve spent years working directly with mills to understand where thermal fluid systems fail and why, recognized at PELICE with 10 consecutive years of industry sponsorship and participation.
No. PumpGuard is designed to augment your existing fire protection, not replace it, adding a dedicated, pump-specific layer that a general suppression system isn’t built to provide at the seal itself.
PumpGuard protects the pump seal itself. PumpGuard+ extends coverage to the volute casing as well, with independently zoned suppression that responds to the specific location of a fire.
No. Fire detection is entirely mechanical, so PumpGuard continues to function even during a total plant power failure. Connecting it to a central HMI panel is optional, not required.
If you’ve had a seal failure in the last year without early warning, or it’s been a while since your system had a dedicated fire risk assessment, that’s usually the clearest sign it’s time for one.